Medical & Healthcare Equipment
Cases can be designed for portable diagnostic devices, monitoring equipment, testing kits, handheld instruments, and healthcare accessories requiring organized storage and transport.
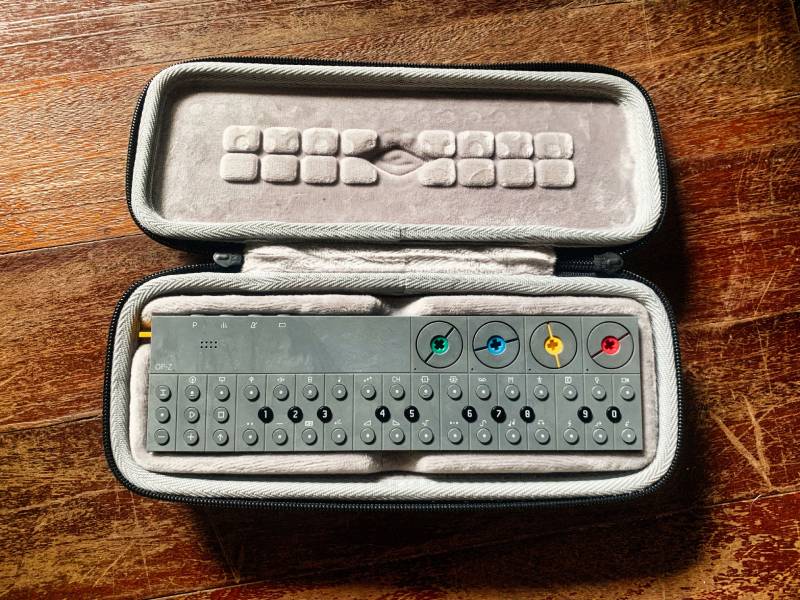
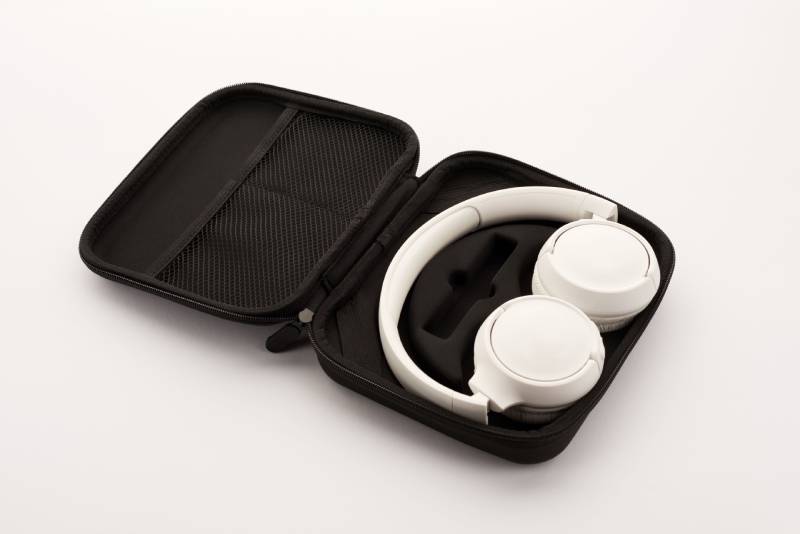
Protection Through Structure
Custom EVA cases combine the lightweight portability of a soft case with the structured protection of a molded enclosure. Using molded EVA (ethylene-vinyl acetate) construction, these cases can be developed around the exact dimensions, contours, and storage requirements of the product they are designed to carry.
Whether protecting medical devices, electronics, diagnostic equipment, tools, instruments, or consumer products, a custom EVA case provides a tailored fit that helps reduce movement during storage and transport. Interior layouts can incorporate custom-cut foam, molded cavities, retention straps, pockets, and accessory compartments to support both protection and organization.
Molded Construction Advantages
Unlike many traditional carrying solutions, EVA cases can be molded into application-specific shapes that closely follow the profile of the product inside. This allows manufacturers to create organized storage environments that improve presentation while helping protect components from impact, vibration, and routine handling.
The final design is developed according to product dimensions, protection requirements, branding objectives, and target production volumes.
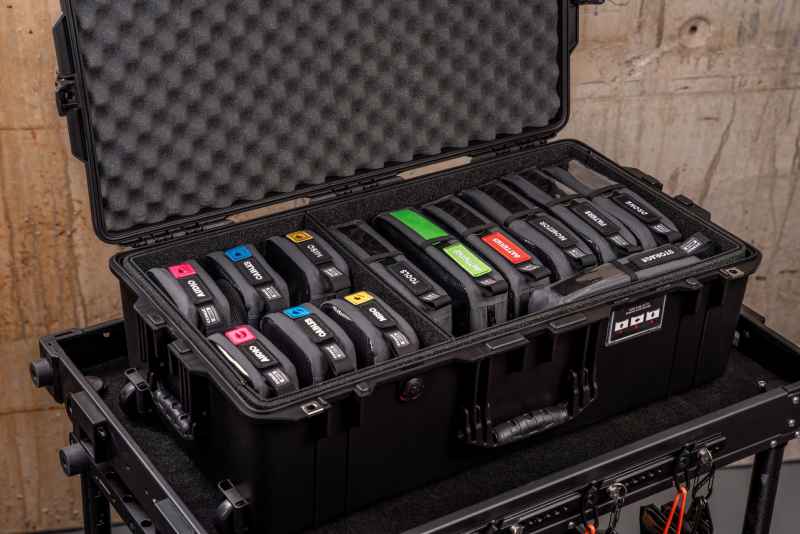
Manufacturing From Concept to Production
Successful EVA case projects begin with a thorough evaluation of the product, how it will be transported, and the protection level required. Factors such as drop exposure, storage conditions, accessory requirements, and user interaction all influence the final design.
Development support may include concept generation, CAD design, sample development, material evaluation, foam design, branding implementation, and production planning. The result is a carrying solution developed specifically for the intended application rather than adapted from an existing case design.
Product Categories Served
Cases can be designed for portable diagnostic devices, monitoring equipment, testing kits, handheld instruments, and healthcare accessories requiring organized storage and transport.
EVA cases may be used to protect testing instruments, calibration equipment, inspection tools, measurement devices, and field-service equipment.
Custom EVA cases are frequently used to protect communications equipment, optics, electronics, testing devices, field instruments, and mission-support hardware during storage and transport.
Products such as tablets, scanners, cameras, communication devices, chargers, and accessories can benefit from custom-molded storage solutions designed around their specific dimensions.
A Custom EVA Case Manufacturing Partner
Custom EVA case projects often require a balance of protection, appearance, manufacturability, and cost considerations. CSE helps guide programs from early design stages through final production while supporting a wide range of product categories.
Common Questions
An EVA case is a protective carrying case manufactured from molded ethylene-vinyl acetate material. EVA provides a combination of durability, cushioning, lightweight construction, and design flexibility.
Yes. Custom EVA cases are typically developed using product dimensions, CAD files, physical samples, or engineering drawings to create a tailored fit.
Options may include molded interiors, die-cut foam inserts, fabric-lined cavities, retention straps, accessory pockets, removable trays, and custom storage compartments.
Yes. Many EVA case programs incorporate custom branding through molded logos, screen printing, labels, zipper pulls, color matching, and packaging enhancements.
@ 2025 CSE Packaging | Powered by : OS Solutions